

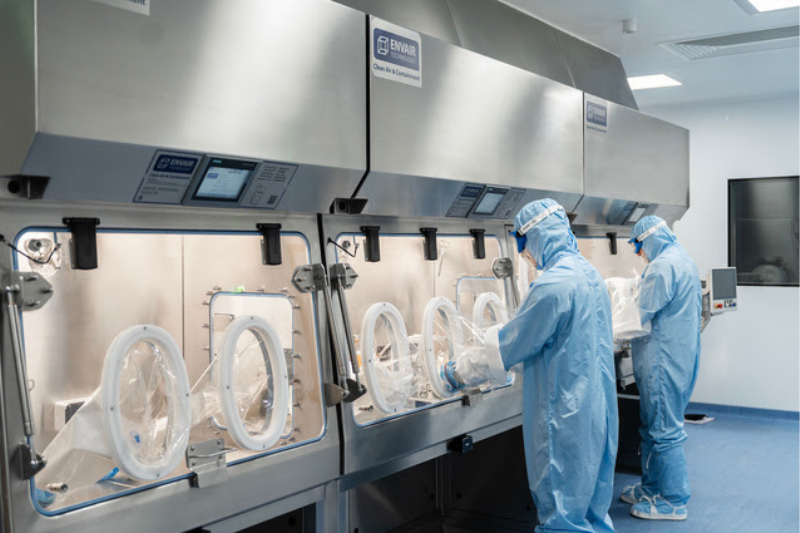
The UK CDMO Upperton has secured approval from the MHRA to manufacture sterile investigational medicinal products (IMPs) at its new facility in Nottingham.
The regulator has approved a variation to Upperton’s existing Manufacturing and Importation Authorisation for Investigational Medicinal Products (MIA(IMP)), extending its scope to cover the company’s new sterile manufacturing facility at Trent Gateway.
The approval enables Upperton to begin GMP manufacture of sterile drug products for early-phase clinical trials, adding sterile clinical supply to its existing formulation development, analytical testing and non-sterile GMP manufacturing services.
New sterile manufacturing capacity
The 7000 sq ft facility has been designed and commissioned in alignment with the revised EU GMP Annex 1 requirements, which set out regulatory expectations for the manufacture of sterile medicinal products.
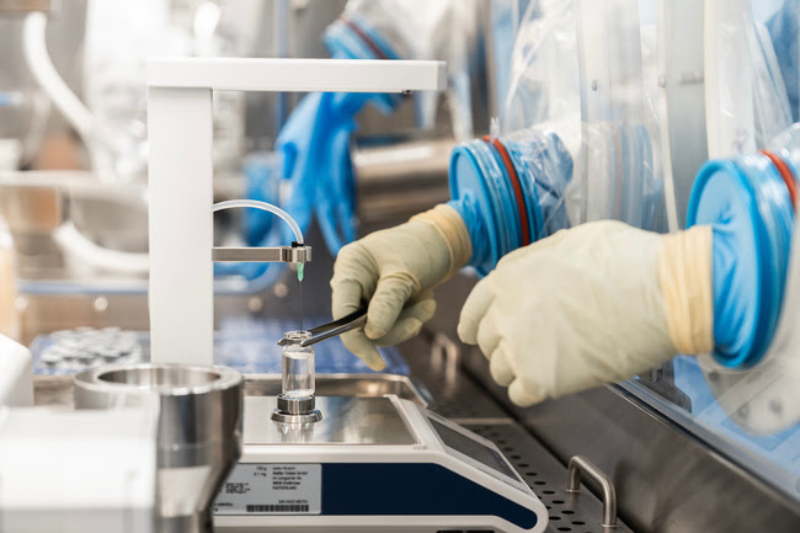 Upperton said that a comprehensive Contamination Control Strategy (CCS) was incorporated from the facility’s design through to qualification and planned routine operation.
The site includes Grade A isolator environments, hydrogen peroxide vapour (VHP) bio-decontamination, dry heat depyrogenation, terminal sterilisation, aseptic processing and independent HVAC systems.
It also incorporates Pre-Use Post Sterilisation Integrity Testing (PUPSIT), which is used to verify the integrity of sterilising filters before use.
According to Upperton, the systems have been selected to minimise operator intervention in critical processing areas while providing flexibility for small-scale GMP manufacturing.
The facility is intended to support both aseptic and terminally sterilised drug products, with a particular focus on early-stage pharma and biotech programmes requiring small-batch sterile fill-finish capacity.
One-site drug development and manufacturing
The sterile facility is located alongside Upperton’s existing 50,000 sq ft development and clinical manufacturing site in Nottingham.
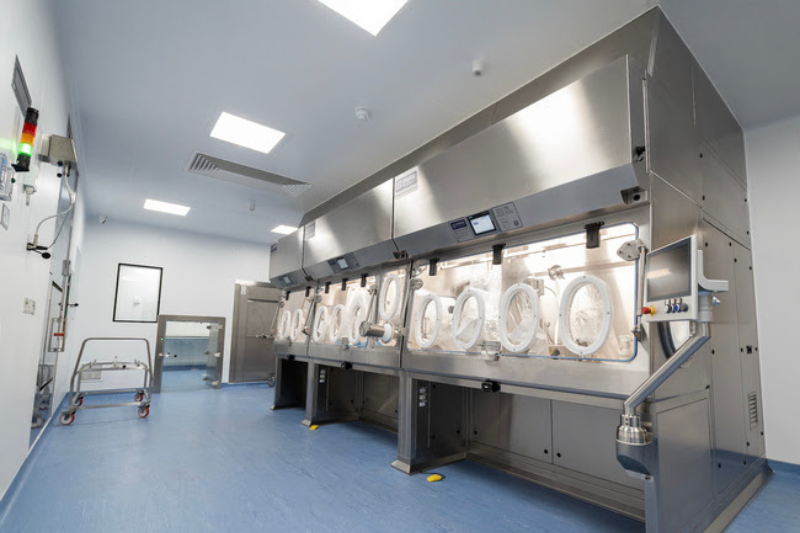 The expanded site allows the company to provide formulation development, analytical testing, non-sterile GMP manufacture and sterile drug product manufacture from a single UK location.
Nikki Whitfield, CEO at Upperton, said the licence reflected the company’s investment in contamination control, quality and patient safety as part of the facility’s design, adding that the "revised Annex 1 framework has significantly raised expectations across sterile manufacturing."
“Securing this licence is a major achievement for Upperton and reflects the dedication and technical expertise of our team."
This approval is one of the first of its kind in the UK, enabling us to provide emerging biotech and with a responsive, high-quality sterile manufacturing service for early clinical development.
Jon Austwick, Director of Quality & Compliance at Upperton Pharma Solutions, said that the facility had been developed using a Quality by Design approach, with contamination control strategies incorporated into the facility, equipment, processes and operator training.
The granting of this licence reflects the commitment of our quality, manufacturing, engineering, validation and technical teams in building a facility that is Annex 1 Compliant, scientifically justified and meets current regulatory expectations.
The licence follows the completion of the facility’s construction, qualification and commissioning, as well as aseptic process simulation activities.
Upperton said the new capability would allow clients to progress from formulation development and analytical work into GMP sterile clinical manufacture without having to move between different manufacturing sites.
The investment forms part of its wider expansion of GMP manufacturing, analytical and quality infrastructure at the company's Nottingham operations.


