For many years, a tablet or capsule checkweigher was viewed primarily as a piece of production equipment. Product went in. A weight was measured. Acceptable and unacceptable units were separated. A batch report might then be printed or exported.
That description is becoming increasingly inadequate.
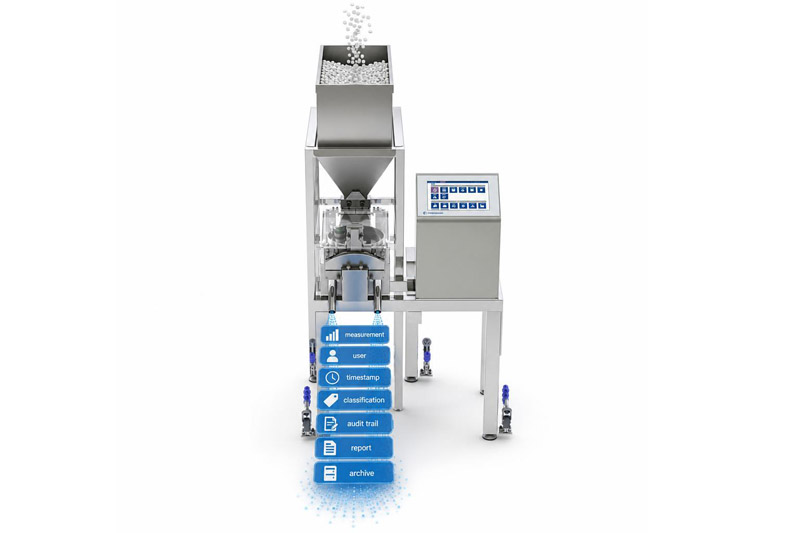
Modern pharmaceutical checkweighers can create thousands, sometimes hundreds of thousands, of electronic records during a single batch. They associate those measurements with products, users, timestamps, limits, classifications, alarms, configuration settings and operator actions.
Those records may subsequently support investigations, process decisions, batch recovery, validation activity or quality review.
At that point, the conversation is no longer only about weighing.
You are operating a computerised GMP system that happens to weigh tablets and capsules.
This changes what manufacturers should expect from the equipment — and what they should ask of the supplier.
This is an excerpt of the complete article - to download the complete PDF - CLICK HERE